Cold Storage Is a Facility. Cold Chain Is a Process.
Why the Difference Determines Whether Your Product Arrives Intact
It is easy to confuse the two, and the confusion is expensive. Cold storage is a facility: a building with refrigerated rooms held at controlled temperatures. Cold chain is a process: the unbroken sequence of controls that keeps a temperature-sensitive product within its required range at every step from origin to final delivery, including all the moments when it is not sitting in a warehouse.
A company can have excellent cold storage and still fail at cold chain. The refrigerated rooms can be perfectly validated while product is compromised during receiving, during an airport transfer, during a customs delay, or in the gap between one provider’s responsibility and another’s. For pharmaceutical, biotech, and medical device shippers, understanding this distinction is the difference between choosing a warehouse and choosing a cold chain partner.
| Cold Storage (a facility) | Cold Chain (a process) |
|---|---|
| A cold room and a thermometer | Validated temperature zones with continuous monitoring and documented alarm response |
| Product held at the right temperature while it sits | Product kept in range at every transfer, handoff, and clearance step, not just in storage |
| Space measured in square feet | Controls measured in unbroken chain of custody and complete documentation |
| A place product goes | A process product moves through, with accountability at every step |
This article walks through what a genuine cold chain process requires, step by step, so that a life sciences company evaluating a provider can look past square footage and refrigeration capacity to the controls that actually protect product integrity.
1. What Qualified Storage Actually Means
Qualified storage is the foundation, but the word qualified is doing a great deal of work that a marketing description often glosses over. A qualified cold storage environment is not simply a room that is cold. It is a validated environment: temperature-mapped to confirm uniform conditions throughout the space, equipped with calibrated monitoring, supported by documented procedures for maintaining and demonstrating compliance, and backed by a quality system that meets cGMP expectations.
Qualification means the facility can prove, with documentation, that the storage environment performs as required, consistently, over time, and that it has the systems in place to detect and respond when it does not. A cold room without that validation and documentation is refrigeration, not qualified pharmaceutical storage. The distinction matters the moment a regulator, an auditor, or a client’s quality team asks for evidence.
2. Receiving and Staging Controls
The cold chain is most vulnerable at its transitions, and receiving is the first major transition under a storage provider’s control. When a temperature-sensitive shipment arrives, the window between the vehicle and the validated storage environment is a moment of real risk. Product left on a dock, staged in an uncontrolled area, or slowly processed through receiving can experience temperature excursions before it ever reaches the cold room.
A genuine cold chain process controls this transition deliberately. Refrigerated product moves from the delivery vehicle into temperature-controlled receiving and staging areas without dwelling in ambient conditions. Receiving inspection, including verification of the shipment’s temperature record in transit, happens promptly and under controlled conditions. The product’s condition on arrival is documented before it is accepted into storage. None of this is visible in a facility’s square footage, but all of it determines whether the product is protected during the minutes that matter most.
3. Airport-to-Warehouse Transfers
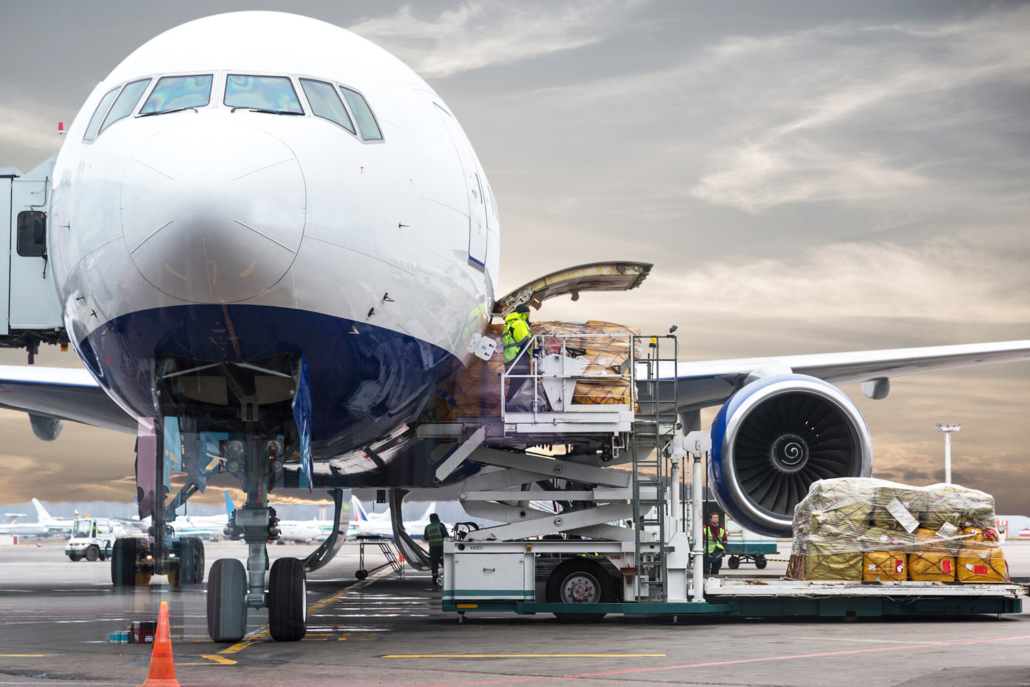
For internationally sourced pharmaceutical product, one of the highest-risk segments of the entire journey is the transfer from the airport to the warehouse. Product that has been maintained in a temperature-controlled environment throughout a transoceanic flight can be compromised in the relatively short ground movement from the aircraft to storage, if that movement is not properly controlled.
A real cold chain process treats this transfer as a controlled step, not an afterthought. Temperature-controlled transportation, appropriate packaging protection, and minimized dwell time on the tarmac and at the receiving dock all matter. This is one of the reasons proximity and integration are valuable: a provider located near the airport, coordinating the customs clearance and the ground transfer and the warehouse receiving as a single operation, can compress and control this segment in ways that a fragmented set of vendors cannot.
The cold chain does not pause between the airplane and the warehouse. If a provider’s responsibility does, that gap is where product integrity is lost.
4. Temperature Monitoring Continuity
Monitoring is only meaningful if it is continuous. A facility that monitors temperature inside its cold rooms but loses visibility during receiving, transfer, or staging has a monitoring gap, and a monitoring gap is a documentation gap. If a product experienced an excursion during an unmonitored segment, no one would know, and no one could prove otherwise.
Genuine cold chain monitoring is continuous across the process, not just within the storage environment. It includes the transit into the facility, the receiving and staging steps, the time in validated storage, and the movement out for distribution. Continuous logging, real-time alerts, and monitoring data that follows the product across each segment are what allow a provider to demonstrate, at any point, that the product remained in range throughout, not just while it sat in a cold room.
5. Customs Delays
For imported product, customs clearance is part of the cold chain, and it is one of the segments most likely to introduce delay. A shipment held for FDA review, flagged for examination, or delayed by a documentation issue does not stop being temperature-sensitive while it waits. Every hour in an uncontrolled holding environment consumes validated shelf life.
This is where the separation between customs brokerage and cold storage becomes dangerous. When the broker and the warehouse are different companies, a customs delay can leave product in limbo, cleared for entry but not yet in controlled storage, with neither party fully accountable for its condition during the wait. A genuine cold chain process anticipates customs delay as a known risk: pre-filing entries to minimize clearance time, maintaining the ability to move product into controlled storage the moment it is released, and, when a hold does occur, having the authority and the facility to place the product into validated conditions rather than letting it sit. Customs is not a separate problem from the cold chain. It is one of its most critical links.
6. Quarantine and Release Status
Pharmaceutical product moving through a compliant supply chain is not simply in storage or out of storage. It moves through defined quality statuses: received, quarantined pending inspection or testing, released for distribution, or rejected. Managing these statuses correctly is a core part of cold chain process control, and it is invisible in any description of a facility’s physical capabilities.
A genuine cold chain process maintains clear segregation and documentation of product status. Quarantined product is physically or systematically separated from released product so that nothing ships before it is authorized. Status changes are documented and controlled. The inventory system reflects the real quality status of every unit at every moment. This is the difference between a warehouse that stores boxes and a quality-managed operation that handles regulated product in accordance with the requirements that govern it.
7. Documentation at Each Handoff
If there is a single thread that runs through every element of a genuine cold chain, it is documentation. Each transition, receiving, staging, storage, status change, and release for distribution, generates records that together form an unbroken chain of custody. That documentation is not administrative overhead. It is the evidence that the cold chain held.
The principle that matters here is ALCOA+: documentation that is attributable, legible, contemporaneous, original, and accurate, along with complete, consistent, enduring, and available. In practice, this means that at every handoff, the responsible party is recorded, the condition of the product is documented, the time is captured, and the record is retained and retrievable. When a regulator or a client’s quality team asks what happened to a specific shipment on a specific day, the answer exists, in full, and can be produced. A cold chain that cannot be documented cannot be proven, and in a regulated industry, what cannot be proven is treated as if it did not happen.
8. Deviation and Excursion Management
No process, however well designed, is immune to the unexpected. Equipment can fail. A shipment can arrive already compromised. A monitoring alarm can trigger at two in the morning. What separates a genuine cold chain operation from a facility with refrigeration is not the absence of deviations. It is the presence of a documented, disciplined process for managing them when they occur.
Effective deviation and excursion management means several things working together. Alarms are monitored continuously and responded to according to defined procedures, not discovered the next morning. When an excursion occurs, it is documented, investigated, and assessed against the product’s validated stability data to determine whether product quality was actually affected. Decisions about affected product are made by qualified personnel with the authority to make them, and those decisions are documented. The client is notified. The root cause is addressed. A provider that can describe exactly what happens when something goes wrong, who is notified, how fast, who decides, and how it is documented, is describing a real process. A provider that cannot is describing a hope.
Ask a prospective provider what happens when a temperature alarm triggers at 2 a.m. The specificity of the answer tells you whether you are buying a process or renting a refrigerator.
9. How to Evaluate a Provider Beyond Square Footage
Square footage and refrigeration capacity are the easiest things to advertise and the least useful things to evaluate. Any provider can state how much cold storage space they have. Far fewer can demonstrate the process controls that actually protect product across the full chain. When evaluating a cold chain partner, the questions that matter are process questions:
- Is the storage genuinely qualified? Ask for evidence of temperature mapping, validation, calibration, and the supporting quality system, not just a temperature range
- How is product controlled during receiving and staging? Ask how product moves from vehicle to validated storage and how that transition is monitored and documented
- How is the airport-to-warehouse transfer handled? Ask specifically about this high-risk segment for imported product
- Is monitoring continuous across the whole process? Ask where monitoring starts and stops, and whether any segment is unmonitored
- How are customs delays managed? Ask whether customs and storage are integrated, and what happens to product during a hold
- How are quarantine and release statuses controlled? Ask how quality status is segregated, documented, and enforced
- What documentation is generated at each handoff? Ask to understand the chain-of-custody records and their completeness
- What is the deviation and excursion process? Ask exactly what happens when something goes wrong, and how fast
The provider whose answers are specific, documented, and process-oriented is offering cold chain. The provider whose answers keep returning to the size and temperature of their facility is offering cold storage. For regulated product, the difference is not academic. It is the difference between product that arrives intact and provable, and product that may be fine but cannot be shown to be.
How Euro-American Worldwide Logistics Approaches Cold Chain as a Process
Euro-American Worldwide Logistics operates validated cGMP cold storage in our Worcester, Massachusetts facility, but the storage is one element of a process we manage end to end. Our licensed U.S. Customs Brokerage and our cGMP warehouse operate under one roof and one team, which means the customs clearance, the receiving, the monitoring, and the storage of an imported pharmaceutical shipment are coordinated as a single, accountable process rather than a series of handoffs between separate companies.
Cleared product moves from customs directly into validated storage without an unmonitored gap. Temperature monitoring is continuous. Product status is controlled and documented. And when a deviation occurs, there is a defined process and a team with the authority to act on it. That is what it means to treat cold chain as a process rather than cold storage as a facility.
If you want to evaluate your cold chain against the process controls described here, or discuss how we handle temperature-sensitive product from arrival through distribution, contact our team.

